Best Stevia Extraction Machine for Industrial Manufacturing
Sep 24, 2026
For industrial buyers, choosing the right stevia extraction machinedecides your stevioside yield, purity, and final profit. Traditional hot-water methods are slow, energy-intensive, and leave 30-40% of glycosides in waste leaves. Our advanced ultrasonic stevia extraction machine from Xi’an Bioland Instrument Co.,Ltd. uses cavitation to break stevia leaf cells at 40-60°C, boosting extraction efficiency by 50-500% and cutting time by over 2/3, while preserving natural sweetness without bitterness.
Xi’an Bioland Instrument Co.,Ltd. is a professional manufacturer and solution provider for R&D production and sales of distillation, concentration, reaction, extraction, separation, filtration, purification, crystallization, emulsification, mixing, drying, and ancillary equipment for supporting those chemical process like heating, cooling and vacuum devices. It's been more than 15 years in such field. Our main products include ultrasonic plant extraction machine, Ethanol extraction machine, extraction concentration unit, and more.
Key Specifications for Industrial Stevia Production
Industrial stevia production demands more than just an extractor; it needs a stable, GMP-compliant system that guarantees consistent Reb-A content batch after batch. The core advantage of our stevia extraction machine lies in its integrated design of ultrasonic breaking, low-temperature extraction, and vacuum concentration in one closed loop. Based on our product line at https://www.biolandequip.com/ultrasonic-extraction/stevia-extraction-machine, this configuration ensures higher purity, lower solvent loss, and continuous operation for large-scale manufacturing.
High Yield Rate Up to 50-500% Improvement for Maximum ROI
Client pain point is low yield. Many factories using conventional reflux only get 8-10% stevioside from dried leaves, with large residue waste. The industry challenge is that stevia cell walls resist solvent penetration. Our stevia extraction machine solves this with ultrasonic physical effects that cause plant tissue to break or deform, making active ingredients fully released. One client in Southeast Asia increased yield from 9.2% to 16.5% in 35 minutes.
That yield jump directly improves ROI. Because our stevia extraction machine extracts more thoroughly, the same raw material produces more finished product. With motor power 2.7-3.5 KW and evaporation capacity 20-200 kg/h, you can process more batches per day without adding labor, turning waste leaves into profit.
Low-Temperature 40-60°C Extraction to Preserve Stevioside Purity
High temperature creates bitter aftertaste and dark color in stevia extract. Traditional boiling at 100°C degrades heat-unstable glycosides and dissolves excessive pigments and pectins. Our stevia extraction machine operates at best temperature 40-60°C under vacuum -0.05 to -0.09 MPA, protecting sweetness profile and reducing impurities for easier purification.
This low-temperature advantage is proven in our tea extraction machine and Coffee Extraction Machine projects. For green tea, we extract tea polyphenols, aromatic oils, and amino acids at low heat to keep antioxidant activity. The same principle helps our stevia extraction machine produce light-colored, high-purity stevioside that meets food and beverage standards without heavy decolorization.
Intelligent PLC Control with Online Concentration Monitoring
Manual operation leads to batch variation and quality complaints from beverage customers. Our stevia extraction machine features intelligent PLC electrical control system, online concentration monitoring, automatic discharging, and CIP online cleaning. You set solvent ratio, temperature, and time once, and the system executes automatically for repeatable results.
Continuous feeding and discharging make concentration pipelined, continuous, and automated. The stevia extraction machine monitors evaporation temperature 60-100°C, jacket pressure 0.09-0.3 MPa, and system vacuum -0.085 MPa in real time. Operators receive alarms if parameters drift, preventing failed batches and ensuring stable production for export orders.
GMP-Compliant SUS304/316L Construction with CIP Cleaning
Export to Europe and USA requires strict GMP/FDA compliance. Our stevia extraction machine is universally manufactured with SUS304/316L stainless steel, equipped with three-layer insulation, defoamer on top of extraction tank and evaporator, and full CIP online cleaning design. It can work under negative, normal, and positive pressure for water or ethanol extraction.
Our products are also exported to Europe and Southeast Asia and other regions. We have ISO safety guarantee and CE certification give you excellent quality promise. This certification advantage helped a European natural sweetener brand pass their audit using our stevia extraction machine, avoiding costly re-equipment and accelerating market entry.
Comparing Capacity and Performance of Extraction Systems
When scaling from lab to factory, many extraction systems fail to maintain linear performance. Ultrasonic power density drops, heating becomes uneven, and yield collapses. Our stevia extraction machine family is designed for true scale-up, offering five standard models with identical control logic so your pilot recipe directly transfers to industrial output without re-optimization.
50L to 500L Scalable Models Matching Your Production Growth
We offer BL-TN-C50L, C100L, C200L, C300L, and C500L for our stevia extraction machine, covering volumes 50 to 500L. A university or startup can begin with 50L for R&D and small pilot production, validate parameters for extracting stevioside from leaves, stems, and roots, then scale to 500L industrial line with same PLC program.
Technology parameter
Model
BL-TN-C50L
BL-TN -C100L
BL-TN -C200L
BL-TN -C300L
BL-TN -C500L
Volume (L)
50
100
200
300
500
Evaporation capacity (kg/h)
20
50
70
100
200
Motor power(KW)
2.7
2.7
2.7
3.5
3.5
Steam consumption(kg/h)
25
60
90
120
250
System vacuum (MPa)
-0.085
-0.085
-0.085
-0.085
-0.085
Pressure of jacket(MPa)
0.09~0.3
0.09~0.3
0.09~0.3
0.09~0.3
0.09~0.3
Compressed air (MPa)
0.5~0.6
0.5~0.6
0.5~0.6
0.5~0.6
0.5~0.6
Evaporation temperature(°C)
60~100
60~100
60~100
60~100
60~100
This scalable design protects your investment. One client in Mexico started with 100L stevia extraction machine for local beverage supply, then added a 300L unit within eight months as demand grew. Because both machines share structure and operation, training time was zero and production doubled quickly with consistent quality.
Evaporation Capacity 20-200kg/h for Continuous Throughput
Throughput bottleneck is often concentration, not extraction. Our stevia extraction machine integrates extraction and concentration. The evaporation capacity ranges from 20 kg/h for 50L model to 200 kg/h for 500L model, with steam consumption 25-250 kg/h. This matching ensures extract is concentrated into required specific gravity ointment without waiting.
The closed-loop design recycles solvent. Secondary steam from concentration goes through condenser and cooler, becoming condensate that refluxes to extraction tank as fresh solvent. New solvent flows from top to bottom through material layer, dissolving soluble components until extraction liquid becomes colorless. Our stevia extraction machine achieves near 95% solvent recovery.
Ultrasonic vs Traditional Hot Reflux: Time Cut by 2/3
Traditional stevia extraction needs 3-5 hours per batch with multiple boiling cycles. Our stevia extraction machine completes best extraction in 24-40 minutes due to cavitation-enhanced mass transfer. This time cut by over 2/3 means you can run 6 batches per day instead of 2, tripling capacity without extra floor space.
Case: A Paraguayan processor struggled with long cycles and high energy bills. Pain point was limited daily output and dark extract. Solution: Replace old reflux with 200L stevia extraction machine with thermal oil heating option for sites without steam. Actual benefit: Cycle dropped to 38 minutes, electricity down 32%, and extract color improved from brown to light yellow.
Energy Saving and Solvent Recovery Performance Analysis
Energy and ethanol costs determine margin in stevia business. Our stevia extraction machine uses low-temperature ultrasonic extraction, so jacket pressure and evaporation temperature are lower than traditional methods. Vacuum pump maintains -0.085 MPa system vacuum, allowing concentration at 60-100°C, saving steam and preventing thermal degradation.
The main products include ultrasonic plant extraction machine, Ethanol extraction machine, extraction concentration unit, co2 extraction machine, supercritical fluid extraction equipment, essential oil distillation equipment, and more. This portfolio expertise allows our stevia extraction machine to adapt to water extraction for crude glycosides or ethanol extraction for high-purity Reb-A, with solvent fully recovered for next batch.
Factors Affecting Machine Selection for Large-Scale Use
Selecting a stevia extraction machine for large-scale use is not just about volume; it is about matching your raw material, solvent strategy, automation needs, and compliance targets. As a process solution expert, we evaluate your whole workflow to ensure the machine solves real production problems, not just performs lab extraction.
Raw Material Variability: Leaves, Stems, and Roots Processing
Stevia leaves contain highest glycosides, but stems and roots also have recoverable value. Different parts have different fiber density and require different ultrasonic power. Our stevia extraction machine has broad adaptability, not limited by component polarity or molecular weight, suitable for leaves, stems, and roots, and even other botanicals.
This flexibility was proven in ultrasonic extraction mushrooms projects. We extract polysaccharides from Ganoderma lucidum, shiitake mushrooms, and sweet potato with same core ultrasonic system by adjusting parameters. Clients using our stevia extraction machine can therefore switch to mushroom polysaccharide line or goji polysaccharide line in off-season, improving asset utilization.
Solvent Flexibility: Water, Ethanol, and Multi-Function Extraction
Water extraction gives high yield but more impurities; ethanol gives higher purity Reb-A. Ourstevia extraction machine supports both, plus multi-function modes: ultrasonic low-temperature extraction, solvent extraction, ultrasonic normal temperature extraction, Soxhlet dynamic extraction, hot reflux extraction, water precipitation, alcohol precipitation, and percolation.
This multi-function extraction is valuable for diversified factories. The same stevia extraction machine platform is used as tincture extraction machine for ethanol extraction of medicinal herbs, as propolis extraction machine for flavonoids and phenolic acids via ultrasonic-assisted ethanol extraction, and as pigment extraction from plants for orange peel pigment and anthocyanins, betaine, carotenoids, and chlorophyll.
Automation Level and Labor Cost Reduction
Labor shortage and human error cause inconsistent glycoside content. Our stevia extraction machine reduces labor through PLC automation, metering tank, storage tank, liquid pump, filter, and automatic discharge. One operator can monitor two lines via central control cabinet, cutting labor cost by 50% compared to manual reflux.
Application scenario: A Chinese health food company had 6 workers per shift for manual stevia extraction. Pain point: High turnover and batch failure rate 12%. Solution: Install 300L stevia extraction machine with online concentration monitoring and automatic cleaning. Actual benefit: Staff reduced to 2, failure rate dropped to 1.5%, and annual labor saving exceeded $45,000.
Compliance and Certification Requirements for Export Markets
If you export to EU, US, or Japan, equipment must meet GMP, FDA, CE, and ISO standards. Our stevia extraction machine complies with pharmaceutical GMP and food HACCP requirements, with documentation support for validation. The stainless steel contact parts, three-layer insulation, and CIP system ensure no cross-contamination between batches.
We also apply this compliance to other lines like Chilli Oleoresin Extraction Plant for capsaicin and chili oleoresin, extraction of flavonoids from ginkgo leaves, bamboo leaves, chrysanthemum, and lotus leaves, and ultrasound assisted extraction of quercetin from larch, celery, mulberry leaves, and sophora japonica. This track record gives confidence that our stevia extraction machine will pass your audits.
Equipment Design for Stable Production Operations
Stable 24/7 operation requires robust mechanical design, clear working principle, and easy maintenance. Our stevia extraction machine is engineered for continuous industrial use, not just laboratory demonstration, with components selected for durability and safety in food and pharma environments.
Core Structure: Ultrasonic System, Extraction Tank, and Concentration Unit
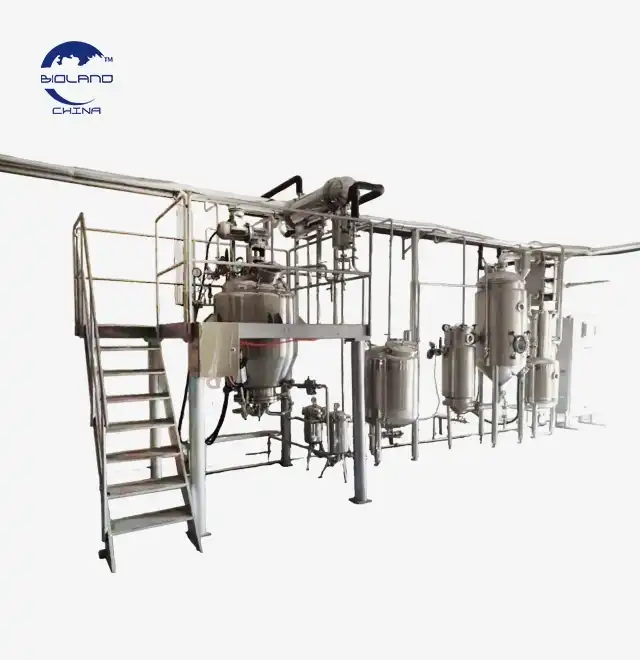
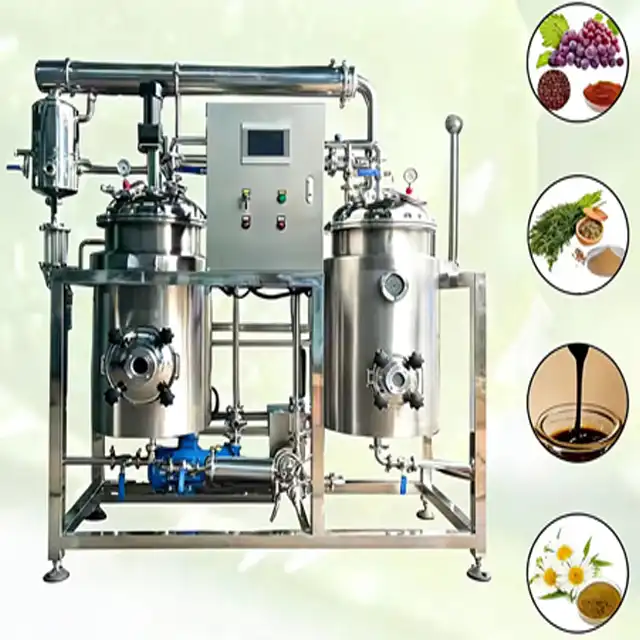
The stevia extraction machine structure consists of ultrasonic system, extraction tank, tubular heater, evaporator, condenser, oil separator, oil receiver, liquid pump, metering tank, storage tank, filter, vacuum pump, and distribution cabinet. Extraction tank and evaporator top vapor outlets both have defoamer to prevent overflow and product loss.
For units without steam heating, we can add thermal oil heating system. All tanks use SUS304/316L with sanitary fittings. This industrial-grade construction ensures our stevia extraction machine runs stably for years, even with corrosive ethanol solvents, reducing downtime and maintenance costs for large-scale manufacturing.
Working Principle: From Feeding to Vacuum Concentration and Reflux
The operating principle of our stevia extraction machine involves specific steps. First, the stevia raw material is loaded into the extraction tank, and a solvent—such as water or ethanol—is added at a ratio determined by the production process. Set extraction temperature per need, typically 50°C, and start ultrasonic extraction per SOP for 24-40 minutes.
After extraction, open pipeline valves in order, pump liquid into concentration tank for vacuum concentration. Set concentration temperature, keep vacuum -0.05 to -0.09 MPA. Secondary steam condenses and returns to extraction tank as new solvent, forming reflux extraction until complete dissolution. Concentration continues until required specific gravity ointment, while colorless liquid in extraction tank can be reused.
Safety Design and Easy Operation & Maintenance for 24/7 Operation
Safety is critical for ethanol extraction. Ourstevia extraction machine includes explosion-proof options, pressure relief valves, and PLC interlocks that stop heating if vacuum fails. The CIP online cleaning system cleans tanks, pipelines, and condenser automatically after each batch, preventing buildup and microbial contamination.
Maintenance is simple. Filters are quick-release, seals are food-grade, and ultrasonic transducers are modular for easy replacement. We provide operation manual, video training, and lifetime maintenance. Clients can schedule Factory Acceptance Test at our facility once goods are ready, testing their own stevia leaves on our stevia extraction machine before shipment.
Multi-Purpose Capability Beyond Stevia for Higher Asset Utilization
Smart investors choose equipment that earns money all year. Our stevia extraction machine is also ideal for plant protein, wheat germ oil, tremella polysaccharide, soybean protein, jujube and goji active substances, rose essential oil, peppermint essential oil, valerian fragrance, caffeine, tea juice, functional food actives like polyphenols and flavonoids, marine fish protein, peony seed oil, and paprika red pigment.
For example, one client uses same stevia extraction machine line for tea polyphenols in spring and stevia in autumn, doubling utilization. Another uses it for pigment extraction from plants in summer. This multi-purpose design, combined with GMP compliance, makes our stevia extraction machine a profit center, not a single-product cost.
Supplier Evaluation for Reliable Extraction Solutions
Choosing a supplier is more important than choosing a machine. A reliable supplier provides process know-how, customization, transparent production, and long-term support. Xi’an Bioland Instrument Co.,Ltd. has been more than 15 years in extraction field, delivering turnkey lines from lab to industrial scale worldwide.
Why 15 Years Manufacturing Experience Matters for Process Solutions
Many traders sell machines without understanding stevia glycoside chemistry. We are manufacturer and solution provider with in-house R&D team. Our TECHNICAL TEAM has senior engineers dedicated to strict quality control and thoughtful customer service. Experienced staff are always available to comply with your requirements and ensure full customer satisfaction.
Our mission is to provide innovative products, valuable insights, comprehensive solutions and real-time support, enabling customers to gain first-class equipment with lowest price, expand businesses, and enhance production capabilities. When you buy our stevia extraction machine, you get 15 years of process data for stevia, tea, chili, mushroom, and propolis lines.
OEM/ODM Customization and 30-Day Fast Delivery Advantage
Standard machines rarely fit existing factory layout. Our company is CE and ISO certified, offering customized equipment and production lines tailored to client requirements, ensuring satisfaction through OEM/ODM services. Whether you need larger oil separator, different voltage, or integration with vacuum spray dryer and freeze dryer, we customize our stevia extraction machine.
Customized products typically have lead time of 30 business days, while non-customized stevia extraction machine is generally ready in 5-7 days. We support sea, rail, and air freight options. This fast delivery advantage helped a US startup launch stevia product three months earlier than competitors who waited 12 weeks for European equipment, at 40% lower price.
After-Sales Transparency: Weekly Video Updates and FAT Support
After-sales anxiety is common when ordering from overseas. We guarantee high quality, supported by excellent pre-sales and after-sales service. Our professional team closely monitors production of your stevia extraction machine, assigning dedicated specialist each week to track progress with photos or videos, keeping you fully informed.
Upon completion, detailed photos or videos are provided for inspection, and shipment is arranged after approval. Alternatively, clients may schedule Factory Acceptance Test at our facility once goods are ready. We provide one-year quality warranty with lifetime maintenance, and all products comply with GMP/FDA standards for your stevia extraction machine.
Proven Success Stories Across Food, Pharma, and Natural Extract Industries
Trust comes from proven cases. Success cases include stevia production line in South America, tea polyphenol extraction line in Fujian, chili oleoresin extraction line in India, mushroom polysaccharide production line in Korea, goji polysaccharide extraction line in Ningxia, natural plant pigment and anthocyanin extraction line in Europe, and propolis line in Brazil.
Application scenario: A Canadian natural color company needed anthocyanin and stevia. Pain point: Two separate suppliers quoted high prices and long lead times. Solution: We delivered one stevia extraction machine based multi-purpose line handling both products with PLC recipe switching. Actual benefit: Saved $70,000 investment, reduced floor space 35%, and achieved payback in 6 months due to price advantage and shared utilities.
Conclusion
For industrial manufacturing, the best stevia extraction machinemust deliver high yield, low-temperature purity, scalable capacity, and GMP compliance in one automated system. Our ultrasonic stevia extraction machine achieves 50-500% higher efficiency in 24-40 minutes at 40-60°C, with 50-500L models, PLC control, and full solvent recovery. Backed by 15 years expertise, CE/ISO certification, and turnkey support, it transforms stevia processing into a profitable, future-proof operation.
FAQ
Q1: What yield can I get with your stevia extraction machine?
A: Typically 50-500% higher than hot reflux. Clients increase from 9% to 16.5% stevioside in 35 minutes at 40-60°C.
Q2: Can the same machine extract leaves, stems, and roots?
A: Yes. Our stevia extraction machine handles leaves, stems, roots, and other botanicals like mushrooms and tea via adjustable ultrasonic power.
Q3: Is the equipment GMP and CE certified?
A: Yes. Built with SUS304/316L, CIP cleaning, ISO and CE certified, fully compliant with GMP/FDA for food and pharma.
Q4: What is delivery time for a customized system?
A: Standard stevia extraction machine ships in 5-7 days; customized OEM/ODM lines in 30 business days with weekly video updates and FAT.
Q5: Does it support both water and ethanol extraction?
A: Absolutely. It supports water, ethanol, and organic solvents with integrated concentration and 95% solvent recovery.
Partner with Bioland Instrument for Your Stevia Production Success
Ready to maximize your stevia yield and cut production time by 65%? Bioland Instrument is your process difficulty solution expert, not just equipment seller. Our stevia extraction machine offers CE/ISO certified quality, GMP-compliant design, 50-500L scalable capacity, PLC automation, price advantage, and proven success across stevia, tea, chili, and mushroom lines. We provide OEM/ODM customization, 5-7 day fast delivery, weekly progress videos, FAT, one-year warranty, and lifetime maintenance. Contact our technical team today atinfo@biolandequip.comfor free process evaluation, customized layout, and quotation. Let’s build your high-profit stevia line together.
References
1. Gasmalla, M. A. A., Yang, R., Amadou, I., & Hua, X. Stevia rebaudiana Bertoni: An alternative sugar replacer and its application in food industry.
2. Periche, A., Castelló, M. L., Heredia, A., & Escriche, I. Influence of extraction methods on the yield of steviol glycosides and antioxidants in Stevia rebaudiana extracts.
3. Jaitak, V., Kaul, V. K., Bandna, B., Kumar, N., Singh, B., & Kaul, V. K. Ultrasonic assisted extraction of stevioside and rebaudioside-A from Stevia rebaudiana.
4. Koubaa, M., Roselló-Soto, E., Šic Žlabur, J., Režek Jambrak, A., Brnčić, M., Grimi, N., & Barba, F. J. Current and new insights in the sustainable and green recovery of nutritionally valuable compounds from Stevia rebaudiana Bertoni.
5. Alupului, A., Calinescu, I., & Lavric, V. Ultrasonic vs. microwave extraction intensification of active principles from medicinal plants.
6. Žlabur, J. Š., Voća, S., Dobričević, N., Brnčić, M., Dujmić, F., & Brnčić, S. R. Optimization of ultrasound assisted extraction of functional ingredients from Stevia rebaudiana Bertoni leaves.
The reactor is beautifully mirror-polished and fully complies with GMP requirements for the pharmaceutical industry. The performance is excellent! Overall, we are very satisfied! We also provided with some feedback on our process improvements, which we hope will be helpful.
2024-04-09
Laboratory
Excellent and professional service. Always reply our questions very fast. All reactors and chiller we received are good too.
2024-02-15
Research Institute
Quality is beyond our expectation actually. After we got the extraction equipment and started using it, the performance was beyond our expectation. Very easy to use and very efficient to run. Service always respond us very quickly. Was also very helpful to help us. Thanks Bioland team. Very happy to work with you.
2023-11-20
Biotech Company
We are happy about the new purchase as always. Equipment and services are both good.
2023-08-05
Instrument Lab
This is the second order with Bioland instrument and everything is good as the first dateText.
2023-05-12
Global Trading Partner
Bioland instrument team is very helpful and professional. The sales helped us select the right equipment for our application, and their logistics people handled the transportation and customs declaration for our shipment. All that saved us a lot of work.