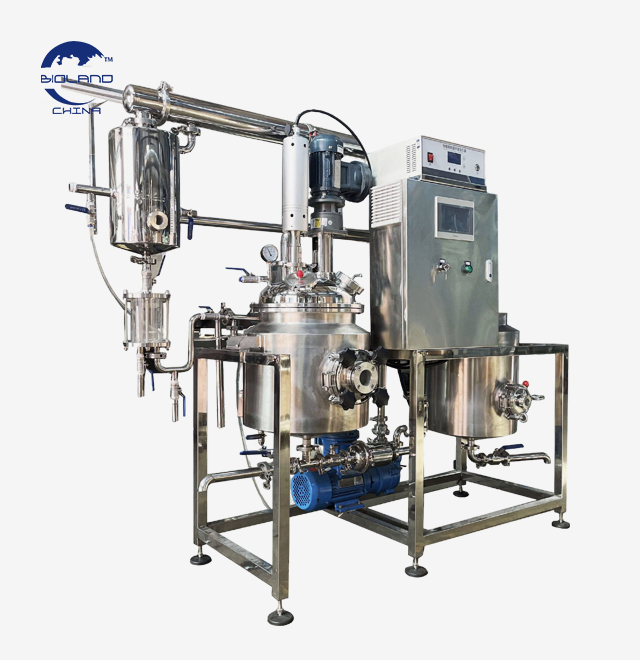
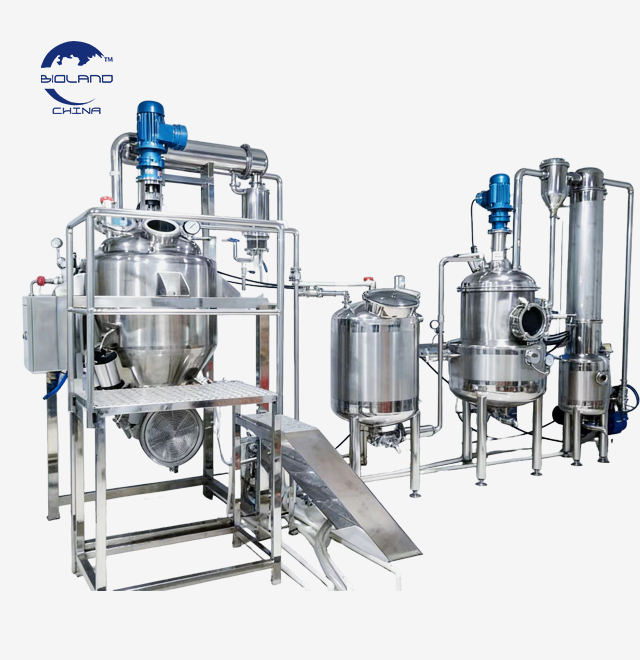
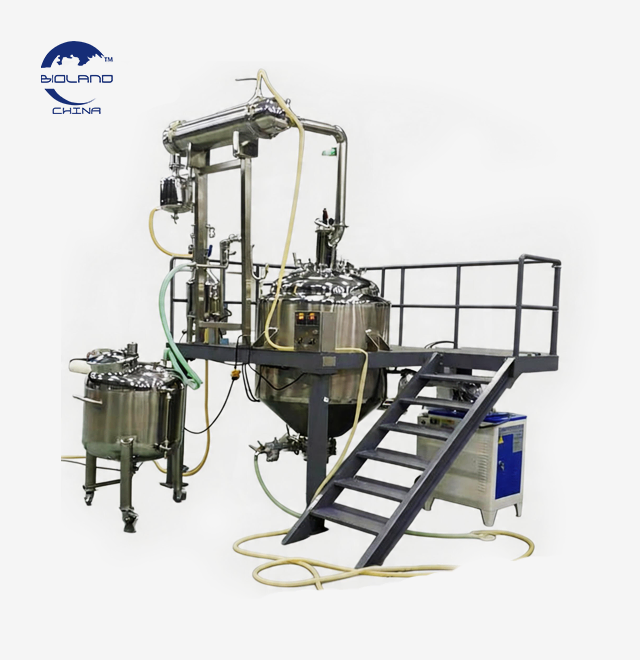
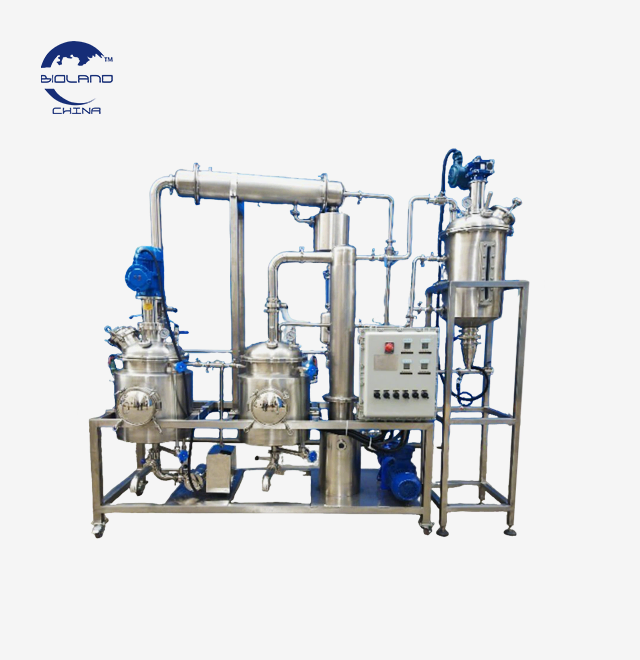
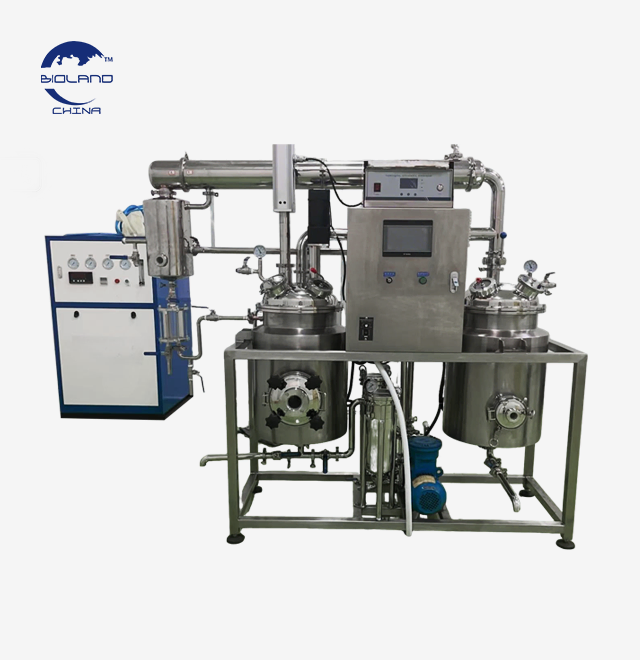
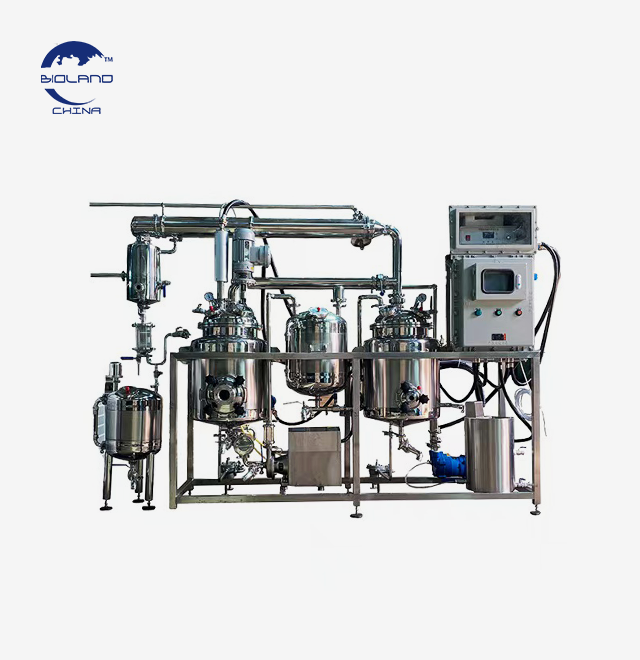
Ultrasound Assisted Solvent Extraction Equipment — Industrial-Grade Solution for High-Yield Bioactive Extraction
Xi'an Bioland Instrument Co., Ltd. provides ultrasound assisted solvent extraction equipment specifically for pharmaceutical, food, and cosmetic manufacturers. Operating frequency covers 20–100 kHz, with extraction efficiency improved by 50–500% compared to traditional methods. The equipment is certified to CE, ISO, UL, SGS, ATEX, and IEC, compliant with GMP specifications, and supports full PLC automatic control and OEM/ODM customization. Standard models ship within 5–7 business days. With 15 years of manufacturing experience, we have served customers in 40+ countries worldwide.

Key Features & Benefits
50-500% Additional Extraction Yield
Acoustic cavitation generates micro-bubbles that explode instantaneously, breaking through the plant cell walls and greatly increasing solvent penetration and mass transfer efficiency – no high temperatures required. Data available upon request from independent third-party laboratories.
Multi-Process Support: SD, UAE, OSE
Each unit can perform three processes: steam distillation, ultrasound-assisted extraction and organic solvent extraction, and may be adjusted for different raw materials and target compounds, so unnecessary investment in equipment is reduced.
Full Explosion-Proof Configuration (ATEX Certified)
ATEX certified generators and transducers dealing with flammable solvents like as ethanol and n-hexane are run with an inert gas protection mechanism, to comply with hazardous area safety requirements and to safeguard the safety of operators.
Twin Ultrasonic And Condenser Modules For High Productivity
The dual-module design maintains a constant cavitation energy density (W/L) in large-volume batches and efficiently solves the energy attenuation problem from laboratory to industrial production.
PLC Automation – Reliable Batch-to-Batch Consistency
The PLC system provides accurate control of ultrasonic time, duty cycle, temperature set points and pump sequences avoiding human operational errors and providing very consistent extraction parameters for each and every batch while meeting GMP batch record standards.

How It Works?
The basic idea of ultrasound aided solvent extraction is not complicated; high intensity sound waves generate millions of tiny bubbles in the liquid. These bubbles collapse instantaneously, generating huge shear stresses and micro-jets that physically rupture plant cell walls, enabling solvent to deeply enter into intracellular areas.
This "sponge-effect" repeatedly compresses and stretches the biological raw material, efficiently releasing alkaloids, flavonoids, polyphenols, essential oils and other active chemicals. Compared to Soxhlet extraction or maceration, extraction time can be decreased from hours to minutes and solvent consumption can be lowered by up to 50%.
The jacketed cooling system keeps bulk temperature at all times. Pulse mode (on/off cycling) also removes localised heat, avoiding degradation of heat sensitive chemicals such as artemisinin and anthocyanins.
Technical Parameters
|
Technology parameter
|
|
Model
|
BL-TN-C50L
|
BL-TN -C100L
|
BL-TN -C200L
|
BL-TN -C300L
|
BL-TN -C500L
|
|
Volume (L)
|
50
|
100
|
200
|
300
|
500
|
|
Evaporation capacity (kg/h)
|
20
|
50
|
70
|
100
|
200
|
|
Motor power(KW)
|
2.7
|
2.7
|
2.7
|
3.5
|
3.5
|
|
Steam consumption(kg/h)
|
25
|
60
|
90
|
120
|
250
|
|
System vacuum (MPa)
|
-0.085
|
-0.085
|
-0.085
|
-0.085
|
-0.085
|
|
Pressure of jacket(MPa)
|
0.09~0.3
|
0.09~0.3
|
0.09~0.3
|
0.09~0.3
|
0.09~0.3
|
|
Compressed air (MPa)
|
0.5~0.6
|
0.5~0.6
|
0.5~0.6
|
0.5~0.6
|
0.5~0.6
|
|
Evaporation temperature(°C)
|
60~100
|
60~100
|
60~100
|
60~100
|
60~100
|
Construction & Materials
- Contact surface material: Standard industrial-grade stainless steel; optional 316L stainless steel for pharmaceutical-grade or corrosive material handling
- Ultrasonic probe (Sonotrode): Titanium alloy, combining corrosion resistance and high acoustic transmission efficiency; service life of 1–3 years under high-solid-content conditions, with periodic resonance frequency calibration service included
- Jacketed vessel: Precision temperature control design, supporting stable extraction quality during continuous operation
- Explosion-proof configuration: ATEX-certified components + inert gas protection interface, suitable for hazardous areas Zone 1/Zone 2

Why Choose Xi'an Bioland
15 years focused on ultrasound assisted solvent extraction and separation equipment manufacturing, exported to 40+ countries, serving over 500 pharmaceutical and food enterprise customers.
Core differences from similar suppliers:
| Comparison Dimension |
Xi'an Bioland |
General Equipment Suppliers |
| Process Support |
SD + UAE + OSE three-in-one |
Usually single process |
| Explosion-Proof Certification |
Full ATEX configuration |
Optional or unsupported |
| Lead Time Transparency |
Weekly photo/video progress updates |
Feedback on request |
| Acceptance Method |
FAT factory acceptance + shipment confirmation |
Mostly shipment confirmation only |
| After-Sales Support |
1-year warranty + lifetime maintenance |
Usually 1-year warranty |
Your dedicated production follow-up specialist tracks the order throughout. All goods must be confirmed by you before shipment, or you may visit the factory in person for Factory Acceptance Testing (FAT).

Services & After-Sales Support
- Pre-sales process matching technical consultation (free)
- OEM/ODM design and engineering support
- Weekly production progress reports (with photos or videos)
- Factory Acceptance Test (FAT, arranged on request)
- One-year quality warranty + lifetime maintenance support
- Spare parts supply (including titanium alloy ultrasonic probes)
- Sea, rail, and air freight options supported

Application Fields
Pharmaceutical & Nutraceutical
Separation and extraction of high value chemicals such as artemisinin, cannabidiol (CBD), alkaloids and flavonoids. Cavitation forces physically destroy rigid cellulose structures without chemical change. Bioactive recovery of extracts confirmed by HPLC and GC-MS as per USP/EP pharmacopoeia standards.
Food & Beverage
Large scale recovery of berry anthocyanins, citrus pectin and olive pomace polyphenols. Especially ideal for deep processing of agricultural by-products, to improve utilisation of resources and reduce production costs, and promote sustainable manufacturing goals.
Cosmetic & Personal Care Industry
Production of oil soluble extracts and essential oils with efficiency. The cavitation-assisted emulsification technology can immediately create stable nano-emulsions during the extraction, leading to the enhancement of the bioavailability of the active cosmetic ingredients, as well as to the reduction of post-processing procedures.

Quality Certifications & Compliance
The equipment holds CE, ISO, UL, SGS, ATEX, and IEC certifications, and is designed and manufactured to GMP and FDA standards.
Compliance support for QC teams:
- Residual solvent analysis complies with ICH Q3C guidelines
- Titanium probe erosion monitoring prevents metal contamination; ICP-MS testing is recommended for verification
- DPPH and ORAC antioxidant activity assays can confirm that cavitation energy has not induced oxidative degradation of target molecules
- Complete batch records and equipment calibration documentation, supporting GMP audits

FAQ
Q: Can the equipment scale from laboratory to industrial production?
A: Yes. The key to scale-up is upgrading from a batch ultrasonic bath to a continuous flow-through reactor to maintain stable energy density (W/L) and cavitation intensity. Our engineering team can provide scale-up process calculation support.
Q: Will the heat generated by cavitation damage heat-sensitive compounds?
A: No. The jacketed cooling system controls the bulk temperature, and pulse mode further dissipates localized heat. Heat-sensitive targets such as artemisinin and anthocyanins have been verified to show no degradation under standard process parameters.
Q: What are the advantages compared to supercritical fluid extraction (SFE)?
A: Ultrasound-assisted extraction requires approximately 20–40% of the CAPEX of SFE equipment at the same scale, with lower operating costs. It is compatible with green solvents such as ethanol and glycerin, and has fewer restrictions on raw material form. Suitable for manufacturers who need to control costs while requiring high extraction yields.
Q: Can flammable solvents be used?
A: Yes. The full explosion-proof configuration includes ATEX-certified generators and transducers, recommended for use with an inert gas protection scheme, suitable for ethanol and other flammable solvent processing scenarios.
Q: What is the service life of the ultrasonic probe?
A: Under high-solid-content conditions, titanium alloy probes typically last 1–3 years, depending on amplitude settings and cumulative operating hours. Periodic resonance frequency inspection is part of the standard maintenance protocol, and we provide probe replacement spare parts.
Q: What certifications does the equipment hold?
A: CE, ISO, UL, SGS, ATEX, IEC — all designed and manufactured to GMP and FDA compliance standards. Certification documents can be provided with the quotation.
Contact Us
Send inquiries or technical questions about ultrasound assisted solvent extraction to info@biolandequip.com — we will respond within 1 business day.